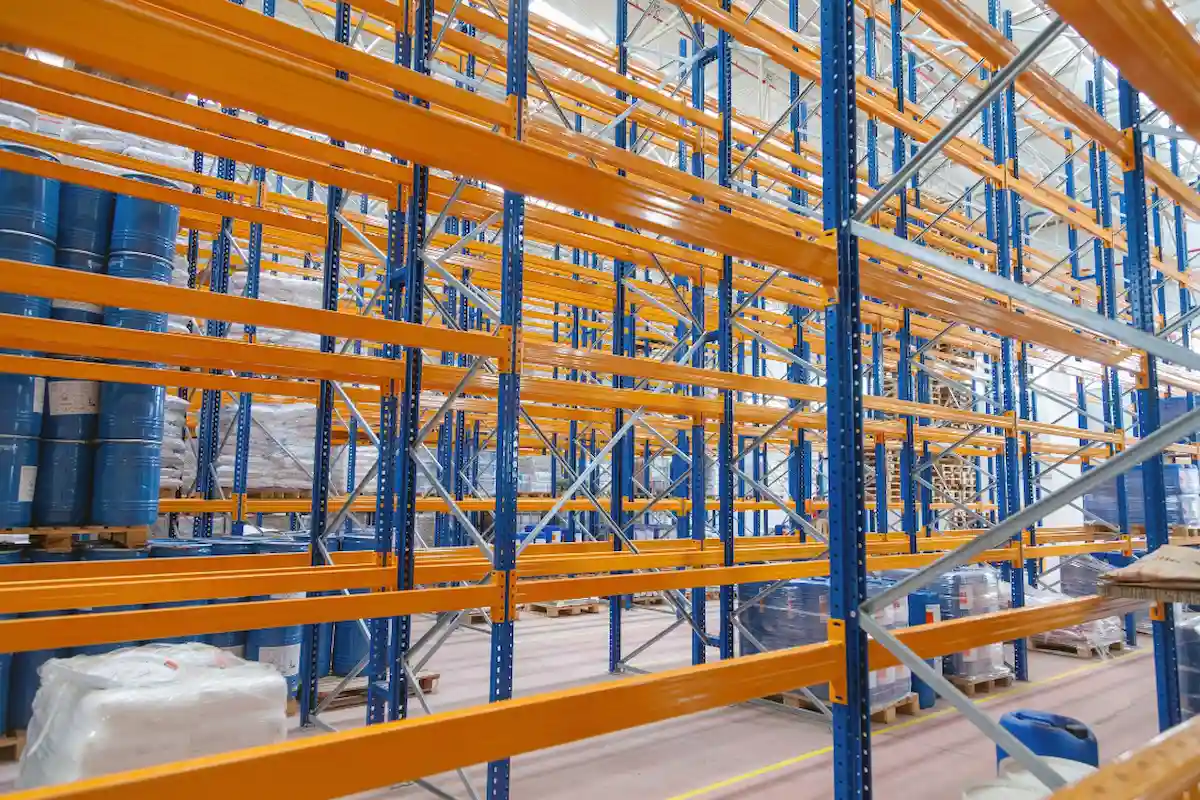
Pharmaceutical Pallet Storage & Medical Racking Systems
Managing pharmaceutical distribution centers, biotech storage facilities, and medical supply warehouses demands strict adherence to international health regulations. Installing certified pharmaceutical pallet storage systems provides the necessary structural foundation to maintain Good Distribution Practice (GDP) and Good Manufacturing Practice (GMP) compliance. These systems are engineered to prevent cross-contamination, facilitate rigorous chemical sanitization, and enforce strict First-In, First-Out (FIFO) batch traceability.
Sanitary Engineering & Cleanroom Structural Standards
High-grade medical racking systems and cleanroom racks are specifically manufactured for controlled cleanrooms and sensitive medical environments:
- Corrosion-Resistant Finishes (Stainless & Powder Coated Racks): Manufactured using high-grade AISI 304/316 stainless steel or non-toxic, anti-microbial electrostatic powder coatings that resist harsh medical detergents and frequent chemical washdowns without flaking.
- Hygienic Profile Construction: Components feature smooth, rounded edges and easily removable shelf inserts that eliminate dust traps and prevent microbial growth in dead spaces.
- Strict Batch Expiry Control (FIFO Flow Rails): Integration of high-precision pallet flow rails and roller beds to enforce strict First-In, First-Out (FIFO) stock rotation, mitigating the risk of pharmaceutical batch expiration.
- Optimized Air Circulation: Frame geometries preserve required clearances between pallets and room perimeters, ensuring uniform HVAC temperature control across all stored medicine boxes.
Field Applications in Bio-Pharma & Healthcare Logistics
Specialized pharmaceutical pallet storage architectures serve vital roles across healthcare supply chains:
- Active Pharmaceutical Ingredient (API) Stores: Segregated, highly traceable racking bays designed to isolate raw chemical materials safely.
- Cleanroom Production Facilities: Stainless steel cleanroom racks designed with particulate-free surfaces for active drug formulation zones.
- Cold-Chain Medical Logistics: Seamless integration between hygienic frames and cold storage pallet racking to preserve temperature-sensitive vaccines and biologicals.
- Manual Picking Operations: Lower storage levels can be retrofitted with ergonomic الأعمدة sliding shelves for safe manual extraction of individual medicine boxes.
Safety Compliance & Regulatory Audits
To ensure full compliance during health ministry audits and WHO-GMP inspections, medical storage racks integrate essential protective components:
- Carton Fall Prevention: Heavy-duty pallet rack safety guards and back mesh netting coated with non-corrosive finishes prevent medical cartons and glass vials from falling into rear access aisles.
- Sanitary Base Anchoring: Structural uprights are anchored using stainless steel feet plates and expansion anchor bolts that eliminate rust formation at floor level during daily sanitation procedures.
- Multi-Tier Packing Platforms: Structural medical frames can support rack-supported mezzanine floors equipped with anti-bacterial decking to double sorting and kitting floor space.
الأسئلة الشائعة
Q1: How do pharmaceutical pallet storage systems support GMP and GDP compliance?
They utilize non-particle-emitting, anti-corrosive materials, facilitate seamless chemical washdowns, prevent dust accumulation, and integrate mechanical FIFO flow controls for absolute batch traceability.
Q2: What is the recommended frame finish for racks installed inside pharmaceutical cleanrooms?
AISI 304 or 316L stainless steel is the industry standard for cleanroom environments due to its complete resistance to oxidation and harsh chemical sterilizing agents.
Q3: Can wire mesh decking be used in pharmaceutical warehouses?
Yes. Galvanized or epoxy-coated wire mesh decking panels are widely used because they prevent dust accumulation while allowing full overhead sprinkler water penetration and HVAC airflow.
التصنيع والتوريد الهندسي
We manufacture and supply certified pharmaceutical pallet storage solutions, stainless steel cleanroom racks, and medical distribution systems across Egypt, along with export-ready logistics for healthcare facilities across the GCC region (Saudi Arabia, UAE, Qatar, Kuwait).
Looking to upgrade your medical or pharmaceutical storage facility to full GMP compliance?
Contact our specialized medical engineering department today for CAD layouts, sanitization specifications, and load capacity assessments.